7 Best Ferrule Crimping Tools for Global Buyers
Choosing the right Ferrule Crimping Tool can influence wiring quality, installation speed, and long-term reliability. For global buyers, the decision involves more than price or attractive packaging. Jaw geometry, crimp consistency, handle comfort, conductor range, and replacement support all deserve close inspection.
Electrical termination specialist Dr. Martin Keller explains, “A reliable crimp begins with the correct ferrule, the correct die, and repeatable pressure.” That principle sounds simple. It is often missed. A tool may close smoothly while producing uneven compression inside the ferrule. That hidden weakness can cause loose strands, heat buildup, or difficult maintenance later.
This guide reviews seven Ferrule Crimping Tool options for workshops, control-panel assembly, field service, and industrial maintenance. Each selection is considered through practical details. These include cable-size compatibility, ratchet action, stripping clearance, jaw alignment, and performance after repeated cycles. The review also considers regional availability and after-sales support, because a tool is not truly reliable when spare parts are impossible to obtain.
No single model fits every user. A compact tool may suit electricians working inside crowded cabinets. A heavier ratcheting model may better serve production benches. Some tools feel excellent during the first hour but become tiring during a full shift. That difference matters.
The comparison is useful, but not perfect. User technique, ferrule quality, and conductor condition can change results. Buyers should verify technical specifications before ordering. Small details matter. This is where careful selection prevents expensive rework.
What Ferrule Crimping Tools Do and Where They Are Used
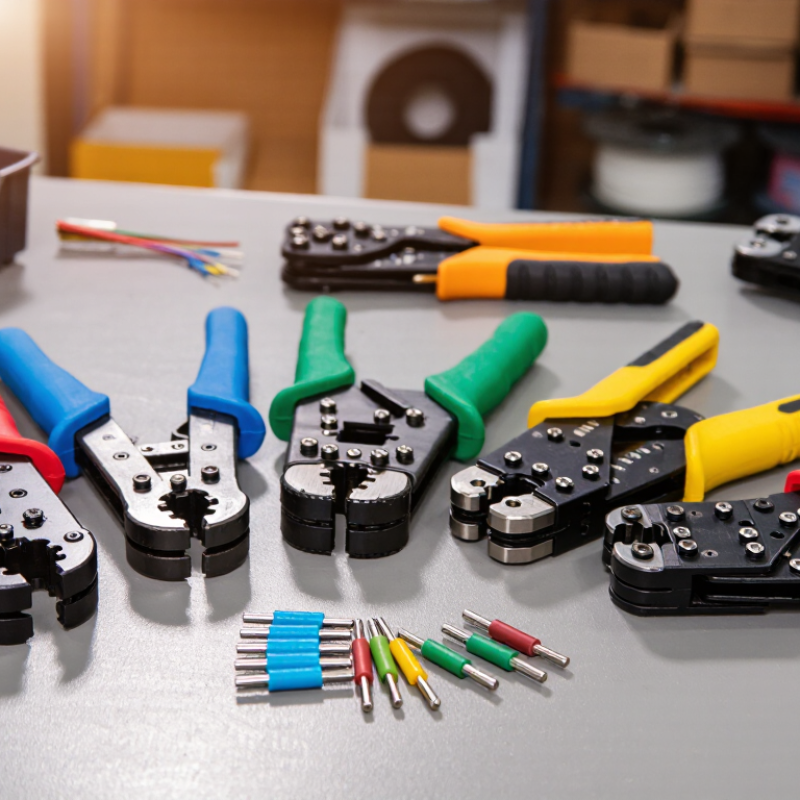
A ferrule crimping tool compresses a metal sleeve around the stripped end of a stranded wire. It prevents loose strands from spreading inside a terminal. The result is a cleaner, more stable connection. Proper crimping also supports consistent insertion into screw-clamp terminals and spring terminals.
Ferrules are widely used in control cabinets, industrial machinery, solar inverters, battery systems, and building automation panels. Grand View Research reported that the global wire and cable market was valued at about USD 201 billion in 2023. More installed wiring means more terminations requiring repeatable workmanship. The International Energy Agency also reported that renewable power capacity additions reached approximately 510 gigawatts in 2023. These systems contain dense cable assemblies, especially inside converters and distribution equipment.
Tool selection should match the ferrule profile, wire range, and required crimp shape. Square and hexagonal crimps behave differently during terminal insertion. A ratcheting mechanism can prevent release before full compression. However, it cannot correct incorrect stripping length or damaged copper strands. The tool is not magic.
Technicians should inspect the finished sleeve for even compression, firm retention, and no exposed conductor beyond the barrel. DIN 46228 is a useful reference for insulated and uninsulated wire-end ferrules. Yet standards do not replace training. A perfect-looking crimp may still fail if the terminal is oversized, the conductor is oxidized, or the tool has lost calibration. That weakness deserves attention in every purchasing decision.
7 Best Ferrule Crimping Tools for Global Buyers: What Ferrule Crimping Tools Do and Where They Are Used
Ferrule crimping tools compress bootlace ferrules onto stranded wire, creating a secure connection for terminal blocks, circuit breakers, PLC wiring, control panels, and industrial equipment. The chart shows seven common metric conductor sizes used with ferrules; tool capacity should always be checked against the required wire range and ferrule profile.
Key Features to Compare Before Choosing a Ferrule Crimper
Choosing among the 7 best ferrule crimping tools starts with the wire range. A suitable crimper should match the ferrule sizes used in your panels, control cabinets, or field repairs. Check whether the tool accepts insulated and uninsulated ferrules. Some models cover broad ranges, while others produce better results within a narrower range.
Crimp quality matters more than appearance. Look for a square, hexagonal, or trapezoidal profile that matches your terminal design. A full-cycle ratchet can prevent incomplete crimps, but it may feel stiff during repeated work. Adjustable pressure is useful when wire strands vary. I prefer clear size markings and replaceable dies, especially when tools travel between countries. Material also deserves attention. Hardened steel supports repeated use, while textured handles reduce slipping in humid workshops.
Test the tool before large production orders. Insert a ferrule, crimp it, and perform a gentle pull test. The wire should not slide out, and the sleeve should remain undamaged. Calibration records, inspection instructions, and spare-part access improve purchasing confidence. However, product descriptions can overstate durability. I once trusted a smooth ratchet too quickly. After several hundred crimps, its pressure became inconsistent. Ergonomics, maintenance needs, packaging quality, and verified technical documentation can reveal more than a polished listing.
Seven Ferrule Crimping Tools for Different Wiring Needs
Choosing a ferrule crimping tool depends on wire size, terminal shape, and working conditions. Seven practical options cover most wiring needs.
A square-profile ratcheting crimper suits control panels and terminal blocks. Its even pressure creates clean contact on common insulated ferrules. A hex-profile crimper works well for thicker conductors and firm cable retention. For mixed wire sizes, a self-adjusting crimper reduces manual setup. It can save time during repeated assembly. A compact hand crimper fits tight cabinets and small repair kits. Its shorter handles improve access, but they may require more hand force. A precision plier-style crimper helps electricians working with thin wires and delicate terminals. I prefer it for short wiring runs where control matters more than speed.
For larger conductors, a hydraulic ferrule crimper provides stronger and more consistent compression. It is heavier, though. A pneumatic crimper suits production benches with frequent, repetitive connections. It offers speed, but needs a clean air supply and proper pressure control. The seventh option is a multi-die interchangeable crimper. It supports several ferrule profiles and reduces tool changes. However, loose dies can create uneven results. Check the die alignment before each batch. Inspect the finished ferrule for full conductor insertion, smooth compression, and no damaged insulation. Tool choice is not always obvious. Test sample wires first, especially when cable strands are unusually flexible or oversized.
How to Match Crimper Designs With Ferrule Sizes
7 Best Ferrule Crimping Tools for Global Buyers
How to Match Crimper Designs With Ferrule Sizes
Choosing a ferrule crimper starts with the ferrule barrel, not the tool’s appearance. Match the die range to the wire size in mm² or AWG. A die designed for 0.5–2.5 mm² may damage a 4 mm² ferrule. Fit matters. Check the ferrule’s metal thickness and insulation collar clearance before crimping. Twin ferrules also need wider entry space than single ferrules.
Square crimps suit many terminal blocks because they create four stable contact faces. Hexagonal crimps work well with round terminal openings and distribute pressure evenly. Four-indent designs can hold conductors firmly in vibration-prone equipment. Ratcheting tools help maintain a complete cycle. Adjustable dies offer flexibility, but they demand careful pressure settings. Do not guess. Excessive force can split thin copper barrels.
In practical assembly work, I inspect the finished crimp from three angles. The conductor should remain visible near the inspection opening, while the ferrule must stay straight. A light pull test can reveal loose compression. I once found a visually neat crimp with insufficient internal contact; appearance was misleading. Measure twice. Buyers should compare the tool’s real working range, die profile, and ferrule compatibility. Published specifications are useful, but samples deserve testing. Different suppliers may label identical sizes differently, creating avoidable errors in international purchasing.
| Rank | Crimper Design | Typical Ferrule Size Range | Crimp Profile | Compatible Ferrule Type | Adjustment and Mechanism | Recommended Wire Applications | Main Advantages | Important Limitations | Selection Rating |
|---|---|---|---|---|---|---|---|---|---|
| 1 | Self-Adjusting Ratchet Crimper Automatic die adjustment for common conductor sizes | 0.25–6 mm² Approximately 23–10 AWG | Square or four-sided compression | Insulated and uninsulated bootlace ferrules conforming to common DIN 46228 sizes | Self-adjusting jaws, full-cycle ratchet, emergency release | Control panels, terminal blocks, industrial wiring, maintenance work | Fast size changes, consistent compression, low operator training requirement | Usually unsuitable for ferrules above 6 mm²; automatic mechanisms may need periodic cleaning | ★★★★★ |
| 2 | Adjustable Square-Profile Crimper Manual die setting with a wider capacity range | 0.25–16 mm² Approximately 23–5 AWG | Four-sided square compression | Single and twin bootlace ferrules, including larger tubular ferrules | Adjustable pressure or indexed die position; ratcheting handle | Power distribution panels, larger control conductors, machinery wiring | Broad size coverage and good terminal compatibility across multiple conductor sizes | Correct die adjustment is essential; incorrect settings can over-compress small ferrules | ★★★★★ |
| 3 | Hex-Profile Ratchet Crimper Six-sided compression around the ferrule barrel | 0.25–6 mm² Approximately 23–10 AWG | Hexagonal compression | Bootlace ferrules and selected tubular terminals designed for hex crimping | Fixed or indexed dies with a full-cycle ratchet | Compact control wiring, instrumentation, automotive harnesses, and terminal cabinets | Even radial compression and strong retention when matched to the correct ferrule | Hex geometry may not fit every spring-clamp or narrow terminal; not ideal for twin ferrules | ★★★★☆ |
| 4 | Compact Precision Crimper Short-handle design for confined spaces | 0.14–4 mm² Approximately 26–12 AWG | Square or trapezoidal compression | Small insulated and uninsulated ferrules for fine-stranded conductors | Manual ratchet with compact handles and controlled release | Electronics cabinets, laboratory equipment, small automation systems, and field service | Easy to carry, suitable for tight panels, and effective on small conductors | Limited leverage and capacity for large ferrules; less suitable for continuous high-volume work | ★★★★☆ |
| 5 | Twin-Ferrule Crimper Designed for two conductors entering one terminal | 2 × 0.25–2 × 6 mm² Combined cross-section depends on the die | Square or trapezoidal compression | Twin bootlace ferrules with a shared insulating collar | Dedicated twin-ferrule cavity or self-adjusting twin-ferrule jaws | PLC terminals, distribution blocks, relays, and compact control cabinets | Maintains two conductors in one ferrule and helps prevent loose strand escape | A standard single-ferrule crimper may not close the wider twin barrel correctly | ★★★★☆ |
| 6 | Hydraulic or High-Force Crimper Intended for large conductor cross-sections | 10–50 mm² Approximately 8–1 AWG | Hexagonal or deep-indent compression | Large tubular ferrules and heavy-duty cable-end ferrules specified for high-force crimping | Hydraulic pump or compound high-leverage mechanism; interchangeable dies may be used | High-current panels, battery systems, industrial power wiring, and large control conductors | Produces high compression force with less operator effort on large ferrules | Heavier, slower, and unnecessary for standard 0.25–6 mm² bootlace ferrules | ★★★☆☆ |
| 7 | Four-Indent Precision Crimper Controlled indentation for specialized ferrules | 0.14–6 mm² Approximately 26–10 AWG | Four-point indent compression | Precision tubular ferrules and selected thin-wall contact sleeves | Fixed precision cavity or interchangeable calibrated dies | Instrumentation, aerospace-style harnesses, test equipment, and vibration-sensitive wiring | Concentrated compression and repeatable results when the ferrule specification is exact | Ferrule and conductor dimensions must be matched carefully; less universal than square-profile tools | ★★★☆☆ |
Global Buying, Quality Checks, and Maintenance Considerations
Global buying demands more than comparing jaw shapes and advertised force.
The 2024 IMARC Group hand tools market report projects steady global growth, with demand supported by electrical installation and maintenance work. That growth makes supplier verification important. Request material certificates, production-batch records, and clear conductor-size ranges. A low price can hide inconsistent dies.
Quality checks should follow recognized technical practice. IEC 60999-1 emphasizes reliable screwless and screw-clamp connections, while applicable regional standards may require separate pull-out, temperature, or flame tests. Inspect the ferrule entry for burrs, then check whether the conductor strands remain fully enclosed. A proper crimp should look even, firm, and free from cracked insulation. Do not trust appearance alone. In field work, I have found that slightly damaged jaws can create weak crimps without obvious marks. A calibrated pull tester is better evidence than hand pressure. Records should include tool identification, inspection date, sample size, and test results.
Maintenance is simple, but often neglected. Remove copper particles after each production shift. Keep the tool dry, lightly lubricate approved pivot points, and store it in a closed case. Never file the crimping cavities. That shortcut changes the profile. Calibration intervals should reflect usage, dust, and impact exposure, not only a calendar date. ISO 9001-based quality systems commonly stress traceability and corrective action, yet smaller buyers may record too little. My own checklist still misses operator fatigue, which can affect alignment late in a shift. Train users to release a jam safely and replace tools showing uneven compression, looseness, or corrosion.
