Quality Mold

How to Choose Mould Components for Global Sourcing

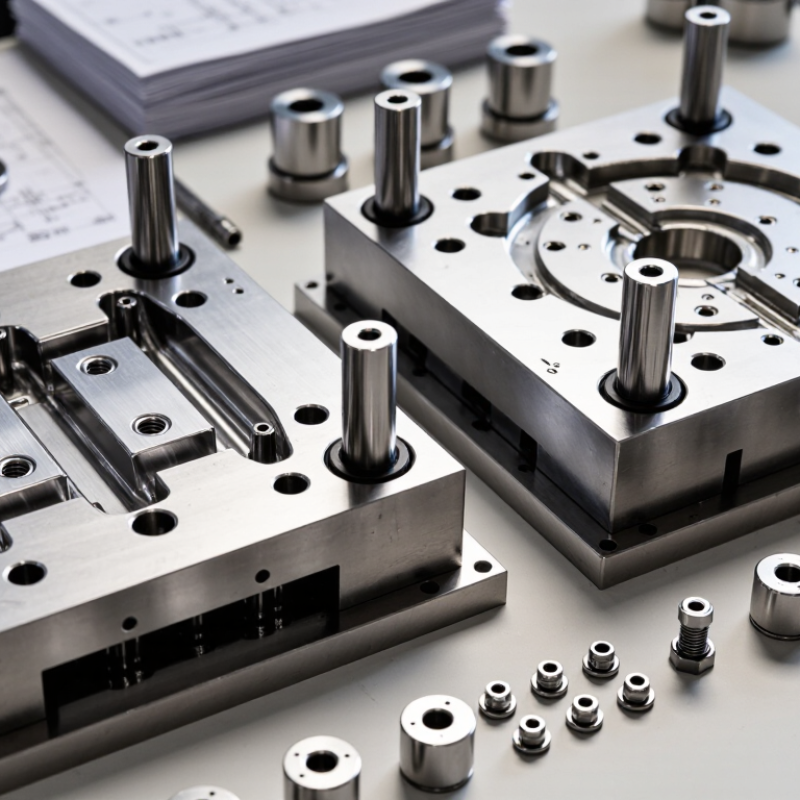
Choosing Mould Components for global sourcing requires more than comparing catalogue prices. The right choice must fit the mould design, material, machine, production volume, and service expectations. A component that looks identical online may differ in steel grade, heat treatment, surface finish, or dimensional control. Those differences often appear later, when an ejector pin wears, a guide pillar binds, or a cooling channel leaks.

John Bozzelli, a respected injection-moulding consultant and founder of Scientific Molding, has repeatedly stressed this practical principle: “The process is the key, not the machine.” The same idea applies to sourcing Mould Components. A reliable supplier should explain how each part supports the process, not only provide a low quotation. Ask for material certificates, inspection records, tolerance data, and replacement lead times. Check whether the supplier understands your mould drawings and production conditions. Small details matter. A 0.02-millimetre mismatch can stop assembly. A poorly finished core pin can mark every moulded part.

Experience also teaches restraint. The cheapest component is not always economical. Yet the most expensive option may bring no measurable benefit. That is where careful comparison is necessary. Review samples, audit communication quality, and test critical parts before full production. I would not trust a supplier based on polished photos alone. Photos hide wear, measurement methods, and delivery problems. A sourcing plan should include approved alternatives, clear acceptance criteria, and realistic logistics. Global purchasing can reduce cost, but only when quality remains visible, measurable, and consistently controlled.
How to Choose Mould Components for Global Sourcing

Define Mould Requirements: Part Size, Material, Tolerance and Cycle-Life Data

How to Choose Mould Components for Global Sourcing

Define mould requirements before comparing suppliers or component quotations. Record the part’s length, width, height, wall thickness, and projected area. Include the resin type, glass content, shrinkage range, and processing temperature. A small change in material can alter wear, cooling, and ejection performance. Do not guess.

Tolerance data needs practical detail. Identify critical dimensions, datum references, surface requirements, and acceptable flash limits. Separate cosmetic areas from functional areas. This prevents expensive precision where it adds no value. Check whether the tolerance suits the part’s function and the moulding process. A perfect drawing can still hide an unclear measurement method.

Cycle-life data should state the expected shot count, operating hours, maintenance intervals, and replacement limits. Describe the production rhythm, such as continuous three-shift operation or occasional batch use. For abrasive materials, specify expected wear on gates, slides, and ejector components. I have seen projects fail because cycle life was treated as a single number. It is not. Ask for inspection records, material certificates, hardness data, and trial results. Keep every revision controlled across time zones. Share a marked sample part when words are uncertain. A short video of the defect can also prevent a long argument. Resist choosing the lowest quotation before comparing assumptions, testing methods, and after-service responsibilities.

Classify Components by ISO 2768 Tolerances and Criticality Levels

How to Choose Mould Components for Global Sourcing

Global sourcing needs a common tolerance language. ISO 2768-1 provides general tolerances for dimensions without individual limits. For example, a 30 mm linear dimension may allow ±0.2 mm under tolerance class “m.” These limits are not automatically suitable for every mould feature. Precision inserts, shut-off surfaces, guide systems, and sealing areas need individual tolerances. The 2024 World Trade Statistical Review reported a 1.2% decline in global merchandise trade volume during 2023. Small specification gaps can therefore create expensive delays across borders.

Classify components by tolerance and criticality. Level A covers mould elements affecting fit, safety, sealing, or product geometry. Assign tighter drawing tolerances, controlled materials, and documented inspection records. Level B covers functional supports, ejector plates, and replaceable wear parts. ISO 2768 medium tolerances may work when testing confirms performance. Level C includes non-functional brackets, covers, and visual surfaces. General tolerances usually reduce unnecessary machining costs.

Do not treat the standard as a shortcut. ISO 2768-2 separates general geometrical tolerances into classes H, K, and L, but it cannot replace engineering judgment. The 2024 ISO Survey of Certifications shows the continuing scale of certified quality systems worldwide, yet certification alone does not prove component accuracy. I have seen drawings that looked complete but lacked datum references. That mistake remains common. A practical sourcing file should include tolerance class, criticality level, measurement method, material condition, and acceptance photographs. Recheck the classification after trial assembly. Some parts behave differently than the drawing suggests.

Compare Steel Grades, Hardness Values and Rated Service Cycles

When choosing mould components for global sourcing, compare steel grade, hardness, and rated service cycles together. A cavity insert may need corrosion resistance, while a large base plate may prioritize toughness and machinability. Do not treat every component as interchangeable. Steel grade influences polishing, thermal conductivity, wear resistance, and repair options at the destination plant.

For many plastic moulds, pre-hardened steel around 28–36 HRC supports practical machining and moderate production volumes. Hardened inserts commonly reach about 44–52 HRC, improving wear resistance but increasing cutting difficulty and tooling costs. The correct value depends on resin abrasiveness, injection pressure, cooling design, and surface finish. A hardness number alone can mislead. I once compared two quotations only by HRC, and the cheaper option had poorer toughness data. That was a useful warning.

Rated service cycles should be treated as an engineering estimate, not a promise. Ask how cycles were measured, including material, cycle time, maintenance, and acceptable wear limits. A mould rated for 500,000 cycles may perform differently with glass-filled resin and aggressive cleaning. Request mill certificates, hardness reports, dimensional inspection records, and a clear replacement plan. Confirm whether hardness is measured on the working surface or a test coupon. Small differences matter. For global sourcing, align these records with local inspection capability and spare-component standards. I still leave a margin for unexpected abrasion, because real production is rarely as clean as a datasheet.

How to Choose Mould Components for Global Sourcing

Compare common mould steel grades by representative hardness and indicative service-cycle planning ranges. Hardness values are shown as midpoints of typical heat-treated or supplied conditions; actual cycle life depends on mould design, material, processing conditions, maintenance and cooling.

Higher hardness generally improves wear resistance, while corrosion-resistant grades can reduce maintenance in humid or chemically aggressive environments. The service-cycle figures are indicative planning ranges rather than universal ratings.

Verify Supplier Capacity, Quality Systems and 100% Inspection Records

Global mould sourcing depends on evidence, not confident promises. Verify the supplier’s machine list, mould capacity, steel procurement, tooling software, and current workload. Request a capacity chart showing machine tonnage, available hours, and planned delivery dates. A supplier may own suitable equipment but lack production time.

Quality systems require closer inspection. The ISO Survey 2022 recorded 1,265,216 ISO 9001 certificates worldwide, but certification alone cannot prove mould-making capability. Check the certificate scope, audit findings, corrective-action records, gauge calibration, and document control. Ask for a sample control plan, process failure analysis, and dimensional report from a comparable project. Practical details matter: cavity measurements, cooling-channel checks, surface-finish readings, and trial-shot records should be traceable to a mould number.

Treat “100% inspection” as a measurable process. Every critical component should have an inspection record, operator identity, equipment number, timestamp, tolerance, and pass-or-fail result. For precision parts, compare the report with calibrated CMM data and material certificates. Keep records linked to each production lot. A 2023 report from the International Trade Centre notes that supply-chain transparency remains difficult for many manufacturers, so missing traceability is a real warning sign. We sometimes over-trust polished certificates. That is a mistake. Review rejected parts, rework history, late deliveries, and open corrective actions. A complete record may still contain errors, but an incomplete record cannot support reliable sourcing.

How to Choose Mould Components for Global Sourcing - Verify Supplier Capacity, Quality Systems and 100% Inspection Records
Component Category Typical Technical Dimensions Common Material and Certification Required Manufacturing Capacity Critical Quality Controls Quality System Evidence 100% Inspection Record Requirements Sourcing Gate
Cavity and Core Inserts Overall size: approximately 50–800 mm
Dimensional tolerance: typically ±0.01–±0.03 mm
Surface finish: Ra 0.2–0.8 µm for polished areas
Pre-hardened or hardened tool steel
Hardness commonly 28–52 HRC
Material certificate with heat number and hardness result
CNC milling, EDM and grinding capability
Work envelope suitable for the largest insert
CMM measurement capability for complex profiles
Parting-line alignment
Shut-off and sealing surfaces
Vent depth and location
Cavity-to-core concentricity
ISO 9001:2015 quality system or equivalent
Approved drawing revision control
Calibration records traceable to ISO/IEC 17025 laboratories
100% dimensional report for all critical datums
CMM or optical measurement files
Hardness and surface-finish records
Serial number or heat-number traceability
Mandatory
Mould Base Plates Plate thickness: commonly 20–250 mm
Flatness: typically 0.02–0.08 mm, depending on size
Alignment-hole tolerance: commonly H7
Medium-carbon steel or pre-hardened mould steel
Material grade must match the approved drawing
Mill certificate required for structural plates
Large-format milling and grinding
Plate size capacity should exceed the mould envelope by a practical machining margin
Through-hole and counterbore machining
Plate parallelism
Guide-pillar and bush locations
Screw-hole pitch and depth
Plate identification and orientation
Incoming material inspection procedure
First-article approval process
Nonconforming-material control and corrective-action records
100% inspection of plate thickness, flatness and hole coordinates
Deburring confirmation
Visual inspection of all machined faces
Measurement report linked to plate serial number
Mandatory
Ejector Plates and Retainer Plates Typical plate thickness: 12–60 mm
Ejector-hole positional tolerance: commonly ±0.02–0.05 mm
Plate parallelism: commonly within 0.03–0.08 mm
Pre-hardened steel or mould-grade alloy steel
Material certificate and hardness record required
Surface treatment documented when specified
CNC drilling, reaming and milling
Capability for long, closely spaced ejector holes
Controlled deburring for sliding interfaces
Ejector-hole location and diameter
Plate movement clearance
Screw-counterbore depth
Parallelism and burr control
Process inspection plan
Gauge calibration records
Documented handling and rust-prevention procedure
100% check of all ejector-hole diameters and locations
100% visual check for burrs, scratches and corrosion
Plate flatness and parallelism report
Mandatory
Guide Pillars and Guide Bushes Common diameter range: 10–80 mm
Diameter tolerance: commonly IT6–IT7
Coaxiality and runout controlled according to drawing
Bearing or hardened tool steel
Typical working hardness: approximately 58–62 HRC for hardened parts
Hardness and plating or coating record where applicable
Centerless grinding and cylindrical grinding
Controlled heat treatment or qualified subcontractor
Roundness and surface-finish measurement
Diameter, roundness and straightness
Surface roughness on sliding areas
Correct fit between pillar and bush
End chamfer and length
Supplier process approval
Heat-treatment verification
Gauge repeatability and reproducibility study for critical gauges
100% diameter and length inspection
Hardness sampling by defined batch plan
Visual inspection for grinding burns, dents and corrosion
Matching record for paired components
Verified
Ejector Pins and Return Pins Typical diameter: 1.5–25 mm
Diameter tolerance: commonly g6 or drawing-specific tolerance
Straightness and tip length controlled for each pin
Hardened tool steel or high-speed steel
Typical hardness: approximately 58–62 HRC
Material and heat-treatment certificates required
Precision centerless grinding
Tip machining, nitriding or coating when specified
Batch traceability for small-diameter pins
Pin diameter and straightness
Tip profile and length
Surface finish on sliding diameter
Correct orientation and quantity
Incoming and final inspection procedures
Batch control and lot identification
Calibration records for micrometers and pin gauges
100% diameter, length and tip-profile verification
100% visual inspection for scratches and burrs
Packing list cross-check against approved bill of materials
Mandatory
Slides, Lifters and Wear Plates Typical travel: 5–150 mm
Functional clearance often specified within 0.02–0.10 mm
Wear-plate thickness and contact area defined on drawing
Pre-hardened or hardened tool steel
Wear plates may use hardened steel or bronze-based materials
Material, hardness and coating documentation required
5-axis or multi-axis machining for angled mechanisms
EDM for tight shut-offs
Assembly trial capability using production-intent components
Slide travel and stop position
Contact pattern and shut-off condition
Wear-plate flatness
Lubrication grooves and access
Design-for-manufacture review
Functional assembly inspection
Corrective-action system for trial-fit failures
100% check of travel, stop position and interference
Contact-blue or equivalent contact-pattern record
Dimensional report for all shut-off surfaces
Assembly photographs or digital inspection evidence
Mandatory
Cooling Inserts and Baffles Cooling-hole diameter: commonly 6–25 mm
Channel position tolerance: typically ±0.10–0.30 mm
Pressure-test requirement defined by mould specification
Mould steel, stainless steel or copper alloy according to design
Material certificate and corrosion-resistance evidence where required
Sealing materials must be compatible with coolant
Deep-hole drilling or gun drilling
Internal passage cleaning
Pressure and leakage testing
Channel diameter and location
Thread quality and sealing surface
Flow direction and blockage control
Leakage and pressure resistance
Pressure-test procedure with calibrated instruments
Cleanliness and foreign-object control
Defined acceptance criteria for leakage
100% pressure or leak-test record for every circuit
100% passage-cleanliness confirmation
Thread and sealing-surface inspection
Circuit identification matched to the cooling layout
Mandatory
Standard Fasteners and Dowel Components Typical thread sizes: M3–M24
Dowel diameter tolerance commonly m6 or drawing-specific
Thread depth and engagement length controlled
Alloy steel, stainless steel or specified mould-grade material
Strength class and surface treatment stated on purchase specification
Certificate of conformity required
Controlled purchasing from qualified sources
Thread gauges and optical inspection
Segregated storage by size and specification
Thread fit and depth
Dowel diameter and length
Head condition and surface treatment
Correct quantity and specification
Approved supplier list
Incoming inspection records
Lot and batch traceability
Counterfeit-component prevention procedure
100% quantity and specification reconciliation
100% visual inspection before assembly
Thread and dimensional sampling according to ISO 2859-1, unless 100% inspection is specified
Risk-Based
Hot-Runner Manifold and Nozzle Interfaces Interface position tolerance commonly ±0.02–0.05 mm
Nozzle seat and gate geometry controlled by mould drawing
Heater and sensor locations verified against the approved layout
Heat-resistant tool steel and approved thermal components
Electrical ratings and material certificates required
No unapproved substitutions for critical thermal parts
Precision EDM and grinding
Electrical continuity and insulation testing
Controlled assembly and preheating test capability
Nozzle-to-gate alignment
Heater resistance and insulation
Thermocouple continuity
Sealing and thermal expansion clearances
Electrical safety test procedure
Assembly work instructions
Calibration records for resistance and insulation instruments
100% resistance, insulation and continuity records
100% interface-dimension verification
Pressure or leakage test where applicable
Serial-number traceability for each assembly
Mandatory
Supplier Final Assembly and Trial Verification Mould size and mass recorded before shipment
Parting-line mismatch commonly controlled to the approved drawing
Trial-shot dimensional results linked to the mould revision
All material and component certificates consolidated
Heat-treatment, coating and subcontract-process records included
Replacement-part list provided
Assembly area with lifting capacity suitable for mould mass
Trial machine or qualified trial partner with matching process range
Packaging suitable for international transport
Mould opening and closing
Ejection and return movement
Cooling and leakage performance
Trial-part dimensions and visual quality
Final inspection checklist
Process capability data for critical dimensions when requested
Corrective-action closure before shipment
Document retention and revision control
100% checklist completion for every mould function
100% record of critical dimensions and utility tests
Trial-shot approval record
Final photographs, packing list and document index
Release Gate
Acceptance values are commonly used reference ranges for global mould-component sourcing. The approved engineering drawing, product specification, applicable material standard and customer quality agreement always take precedence. Critical characteristics should be identified with a ballooned drawing and supported by complete, traceable inspection records.

Evaluate Total Cost Using Lead Time, MOQ, Tooling and Logistics Data

How to Choose Mould Components for Global Sourcing

Evaluating mould components requires more than comparing unit prices. Lead time, MOQ, tooling, and logistics can change the real project cost. A low-priced insert may still delay production by three weeks. That delay can create overtime, storage, and missed delivery costs.

Request a clear lead-time schedule for machining, inspection, and shipment. Check whether the supplier holds standard components locally. Review MOQ against your actual production plan. Excess inventory ties up cash and may become obsolete after a design change. Tooling charges also need careful review. Confirm what the fee includes, such as drawings, trial fitting, corrections, and replacement parts. Ask for dimensional inspection records and material certificates. These details improve purchasing reliability.

Tips: Build a simple cost sheet for every option. Include component price, tooling, freight, duties, handling, and delay risk. Compare suppliers by delivered cost, not invoice value. Add a small contingency for customs checks or transport disruption. I have found that estimates often look precise but hide assumptions. Challenge each assumption. A cheaper option may win on paper and fail during installation. Recheck the calculation after design approval, because even a minor tolerance change can affect machining time, MOQ, and freight volume.