How to Choose Injection Molding Tooling in 2026?
In 2026, choosing injection molding tooling means balancing part quality, production volume, lead time, and the full cost of ownership. A tool that looks inexpensive on a quote can become costly when cooling is uneven, gates leave visible marks, or maintenance stops production. Small details matter. A 0.2-millimeter wall change, a deep rib, or a tight tolerance can affect steel choice, cavity count, and mold design. Buyers should compare suppliers on documented experience, process capability, design support, and clear validation plans—not price alone.
John Beaumont, co-author of a respected reference on runner and gating design, offers a useful principle that can be summarized this way: treat the mold as a complete flow system, not merely a cavity. That perspective helps teams assess how resin travels through runners and gates, fills each cavity, cools, and ejects. Ask for evidence: mold-flow findings, steel specifications, sampling criteria, and a maintenance schedule. Check who owns design changes, too. It is an easy detail to overlook.
The right choice depends on what the part must do in real use. A short pilot run may justify a simpler aluminum tool; sustained production may call for hardened steel and replaceable inserts. Neither option is automatically better. Resin choice, annual demand, cosmetic surfaces, and expected tool life can change the calculation. Suppliers may also disagree, and that is worth examining. Compare their assumptions, request examples from similar parts, and confirm how defects will be measured before approving the tooling. A careful decision now can prevent expensive surprises later.
Define Part Requirements and Production Goals
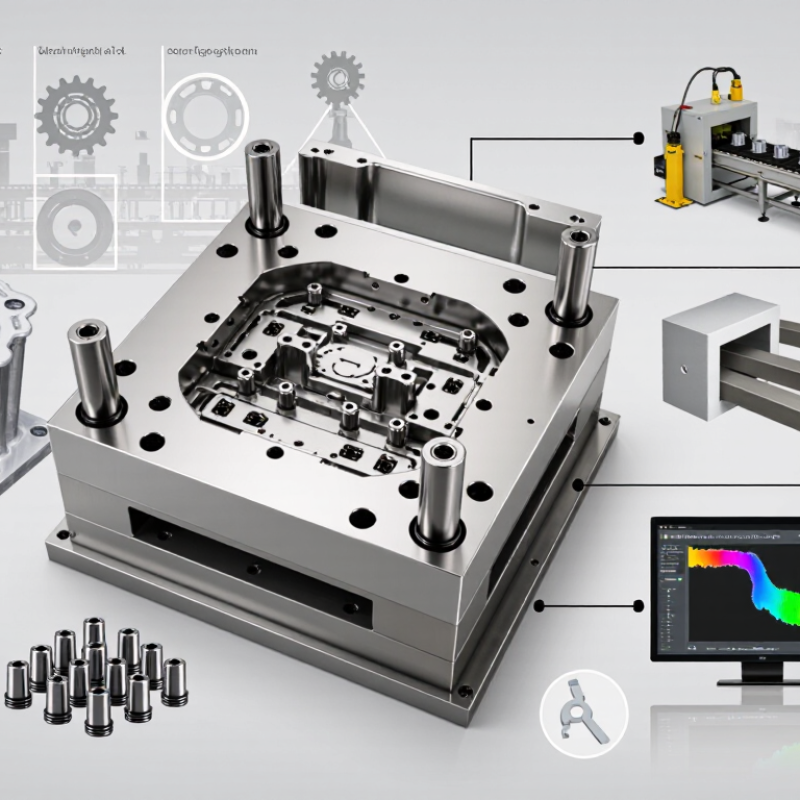
Define part requirements before comparing injection molding tooling. Record the resin, part dimensions, wall thickness, tolerances, surface finish, and any critical fit points. A thin rib or glossy face can affect cooling, ejection, and mold complexity. Set the expected annual volume, target cycle time, product lifespan, and launch date too. Without these figures, a low-cost quote may hide costly compromises.
Grand View Research estimated the global injection molding machine market at USD 10.89 billion in 2023 and projected 4.9% annual growth from 2024 to 2030.
This is machine-market data, not a tooling-cost forecast, but it signals a production landscape where capacity planning matters. Match tool life and cavity count to realistic demand: a single-cavity tool may suit a pilot run, while multi-cavity tooling can improve output at scale. Forecasts are still forecasts. Leave room for uncertainty.
Tips: Send suppliers a dimensioned 3D model, resin specification, and volume range. Ask for a documented quote covering tool life, maintenance, sampling, and cycle-time assumptions. Check those assumptions against the part’s thin sections and visible surfaces; small details can change the plan. I would revisit the forecast before committing to a large tool.
Grand View Research, “Injection Molding Machine Market Size, Share & Trends Analysis Report,” 2024.
Compare Mold Types, Materials, and Cavitation Options
How to Choose Injection Molding Tooling in 2026?
Compare Mold Types, Materials, and Cavitation Options
Tooling choice starts with production volume and part requirements. A prototype mold can help verify fit and surface finish before a larger investment. Aluminum tooling often suits shorter runs and faster changes, while hardened steel can withstand demanding, repeated production. The right choice depends on resin, expected output, and maintenance needs. Abrasive or glass-filled materials may wear cavity surfaces faster. Small batches change the math.
Cavity count affects output, cost, and process control. A single-cavity mold is easier to adjust and can make sense for low demand or complex parts. Multi-cavity tooling produces more parts per cycle, but cavities need balanced filling and consistent cooling. Family molds can form different components together, though mismatched part sizes or fill requirements may complicate quality control. More cavities are not automatically better.
Tips: Ask the toolmaker to review annual volume, resin, tolerances, and likely design changes. Request cycle-time and maintenance estimates, not just the initial tool price. Check that the proposed steel grade fits the material and production target. A small trial run can reveal uneven filling or flash before full production. I would still leave room for uncertainty: real cycle times can differ from early estimates.
How to Choose Injection Molding Tooling in 2026?
Compare mold types, materials, and cavitation options by estimating how cavity count affects production output.
Illustrative output estimate: Assumes a 30-second cycle and 90% effective production time, giving 108 parts per cavity per hour. Actual output varies with part design, resin, mold material, cooling, machine capability, and production conditions. More cavities can increase output, but also require a suitable press and may increase tooling complexity and cost.
Evaluate Toolmakers, Design Support, and Manufacturing Capacity
How to Choose Injection Molding Tooling in 2026?
Evaluate Toolmakers, Design Support, and Manufacturing Capacity
A tooling quote is only a starting point. Ask who owns mold design, who reviews your part geometry, and who will cut, fit, and trial the tool. Request a sample design-for-manufacturing review, with specific notes on wall thickness, draft, gate location, and likely sink marks. Look closely. Useful support identifies trade-offs, not just problems.
Capacity needs evidence. Ask for a recent schedule showing design, machining, sampling, and correction time, then compare it with your launch date. The 2024 workforce report from Deloitte and the Manufacturing Institute estimates that 1.9 million U.S. manufacturing jobs could go unfilled by 2033. That makes backup coverage, skilled operators, and maintenance plans worth checking—not assuming. Ask who can run the press if a key technician is away.
Digital systems help, but they are not proof of reliable delivery. Deloitte’s 2025 Smart Manufacturing and Operations Survey found that 92% of manufacturers see smart manufacturing as a competitiveness driver within three years. For a mold project, ask what that means on the floor: can the toolmaker share current machine status, inspection records, and trial results? A polished dashboard can still hide a bottleneck. Verify claims with a recent tool build, a sample inspection report, and a clear plan for design changes.
How to Choose Injection Molding Tooling in 2026? — Evaluate Toolmakers, Design Support, and Manufacturing Capacity
| Evaluation Dimension | Suggested Weight | Evidence to Request | Practical Acceptance Check | Warning Signs |
|---|---|---|---|---|
| Relevant toolmaking experience | 15% | Examples of molds with comparable part size, resin, geometry, expected production volume, and tolerance requirements. | Confirm the proposed process, mold construction, and inspection plan suit the part’s actual requirements. | Experience is described only in general terms, or examples do not match the part’s complexity or resin. |
| Design-for-manufacturing support | 15% | A documented design-for-manufacturing review covering wall thickness, draft, parting line, gate location, ejection, and likely molding risks. | Review proposed changes with the product team before the mold design is released for manufacture. | Design changes are made without approval, or the review omits how proposed changes affect fit, function, or appearance. |
| Tool design and documentation | 12% | Tool layout, steel and component specifications, cooling and ejection concepts, revision control, and a plan for design approval. | Agree on who owns the design files, how revisions are recorded, and which drawings or models are delivered. | Key design decisions or deliverables are left undefined until after the order is placed. |
| Manufacturing capacity and machine fit | 12% | Available machining and inspection resources, current workload, and the molding machine’s clamping force, shot capacity, and platen limits. | Check that the selected machine can accommodate the mold and the resin’s required shot size and processing window. | Capacity is promised without identifying the relevant machines, schedule assumptions, or production constraints. |
| Quality planning and traceability | 12% | Inspection plan, measurement equipment list, material certifications where applicable, and documented handling of nonconformances. | Define critical-to-quality dimensions, sampling expectations, and the approval process for first molded parts. | Acceptance criteria are vague, or inspection results cannot be linked to the relevant tool or production revision. |
| Sampling and validation plan | 10% | A proposed trial plan stating the sample quantity, resin and colorant, processing conditions, dimensional checks, and reporting format. | Make sure samples are evaluated against an agreed drawing and that adjustments are documented between trials. | Sample approval is treated as a visual check only when dimensional or functional requirements also apply. |
| Schedule and change management | 10% | A milestone-based schedule covering design approval, steel or material procurement, machining, assembly, trials, and corrective work. | Confirm dependencies, approval deadlines, and how scope or engineering changes affect cost and timing. | Only a single delivery date is offered, with no milestones or stated assumptions. |
| Maintenance, repair, and spare parts | 8% | Recommended maintenance tasks, wear-item list, spare-component options, and procedures for repair or design changes. | Agree on the maintenance records and support process needed for the intended production environment. | No maintenance guidance is supplied for components subject to wear or routine replacement. |
| Commercial clarity and risk allocation | 6% | An itemized quotation identifying mold scope, trial scope, exclusions, payment milestones, warranty terms, and ownership arrangements. | Resolve tooling ownership, storage, transfer, and access to design data in the written agreement. | Important charges, ownership terms, or responsibilities are omitted or described inconsistently. |
| Total suggested weighting | 100% | Use the weights as a starting point and adjust them to the part’s risk, production volume, and program requirements. | ||
Scoring method: Rate each dimension from 1 (insufficient evidence) to 5 (strong, verified evidence), multiply the rating by its suggested weight, and compare the weighted results. Treat quoted lead times, tool life, and production capacity as project-specific commitments to verify—not universal benchmarks.
Estimate Total Tooling Costs, Lead Times, and Ownership Risks
Choosing injection molding tooling in 2026 means pricing the whole production path, not just the mold. Request separate costs for design, steel or aluminum, sampling, revisions, maintenance, and freight. Ask whether the quote includes texture, cooling channels, and a defined number of test shots. A low initial price can hide expensive changes later. I still treat unusually low quotes with suspicion; sometimes that may be too cautious.
Lead times depend on part complexity, tool material, and supplier capacity. Get a written schedule with dates for design approval, first samples, and production release. For early validation, additive manufacturing may reduce the need to commit to a production tool immediately. The Wohlers Report 2024 estimated that global additive manufacturing revenues reached $20.035 billion in 2023, an 11.1% annual increase. That growth reflects broader use of the technology, though it does not guarantee a faster or cheaper molded part.
Tips: Put ownership in the purchase agreement. Confirm who holds the tool, who pays for repairs, and whether you can transfer it to another supplier. Specify storage conditions and access to tool records. A mold sitting unused can still deteriorate. Decide who approves modifications before the first cavity is cut.
Verify Tool Performance Through Sampling and Production Readiness
How to Choose Injection Molding Tooling in 2026?
Verify Tool Performance Through Sampling and Production Readiness
A tool is not production-ready because it produces one attractive part. Sampling should use the intended resin, colorant, and process settings, not convenient substitutes. Check critical dimensions across consecutive shots, then inspect for flash, sink marks, short shots, and visible variation. One shot proves little. Record cycle time, scrap, and any manual adjustments; these details can reveal a tool that only works under careful supervision. Agree on acceptance limits before the trial, including which dimensions require tighter control. ISO 20457:2018 provides guidance on tolerances for molded plastic parts, but functional requirements still need to be defined for each product.
Production readiness also means testing a realistic process window. Vary key settings within approved limits and confirm that parts remain acceptable. Measure more than the easiest features. The Plastics Industry Association’s 2023 Size and Impact report estimated the U.S. plastics industry’s 2022 economic contribution at about $548 billion, a reminder of the sector’s scale—not evidence that any individual tool is capable. Keep the sampling record: resin lot, machine settings, inspection results, cycle time, and corrective actions. A clean first run can still mislead. If results depend on unusually slow cycles or frequent operator intervention, pause before sign-off. The uncomfortable question is whether another shift can repeat the same results.
Related Posts
-
Understanding the Essential Role of Injection Molding Tooling in Modern Manufacturing
-
China Top 10 Injection Molding Manufacturers to Learn From
-
2025 Top Digital Innovations in Injection Molding Tooling for Efficient Production
-
2026 Top Injection Molding Mold Types for Global Buyers
-
China Top 10 Plastic Injection Mold Tooling Companies
-
10 Essential Tips for Successful Medical Injection Molding Process